FDM, SLS, and SLA Compared: Picking a Process for Functional Prototypes
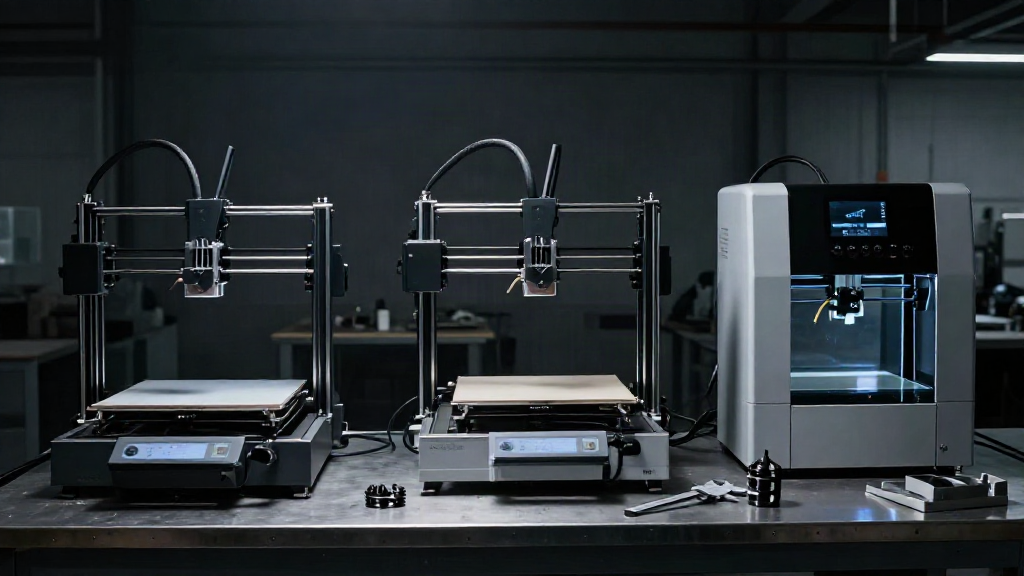
FDM, SLS, and SLA are the three processes behind almost every functional prototype and low-volume production part ordered in Canada today. They are not interchangeable. Each one builds a part a different way, and that difference decides how strong the part is, how fine the detail gets, how smooth the surface comes out, and what it costs per unit at 5, 50, or 500 pieces.
This is the comparison to read before you upload a CAD file. Pick the right process and you get a part that behaves like the real thing on the first try. Pick the wrong one and you pay for a reprint.
The short version
- FDM extrudes molten thermoplastic filament in layers. Best for brackets, enclosures, jigs, and anything that has to take a load.
- SLS fuses nylon powder with a laser, layer by layer, with no support structures. Best for complex geometry, living hinges, and short-run production.
- SLA cures liquid resin with a laser or light engine. Best for fine detail, smooth surfaces, and parts that must look finished.
| FDM | SLS | SLA | |
|---|---|---|---|
| Material | ABS, PETG, PC, TPU, PLA | Nylon (PA12, PA11) | Photopolymer resin |
| Strength | High, but anisotropic | High and uniform | Moderate, brittle |
| Detail | Coarse (0.1-0.3 mm layers) | Medium | Excellent |
| Surface | Visible layer lines | Matte, slightly grainy | Smooth to glossy |
| Supports | Required, removed by hand | None needed | Required, cleaned off |
| Best for | Functional fit and load | Complex, end-use parts | Detail and finish |
FDM: the workhorse for parts that have to work
FDM builds by laying down a bead of melted filament, layer over layer. It is the most widely available and usually the cheapest per part, which makes it the default for early iterations.
The trade-off is direction. An FDM part is strong along the extrusion path and weaker between layers, so a bracket that fails will almost always fail along a layer line. If a part is going to be bolted, loaded, or dropped, orient the print so the load runs along the layers, not across them.
FDM is the right call when you need a rugged prototype that mounts to real hardware, a jig that holds up on the shop floor, or a housing you can tap and assemble. Layer lines are visible, but for a part that is going to be handled and tested rather than photographed, that rarely matters.
SLS: complex geometry, no supports, production-ready
SLS spreads a bed of nylon powder and fuses one cross-section at a time. Because the surrounding powder supports the part, there is nothing to remove and nothing to break off. Overhangs, internal channels, nested features, and interlocking assemblies all print in one piece.
That freedom changes what you can design. SLS parts come out strong and consistent in every direction, which is why the process carries so much short-run production work: nylon is tough, chemically resistant, and machinable, so an SLS part can be tapped, dyed, or bead-blasted after printing.
The surface is matte and faintly grainy, not glossy. If a part needs to look like a molded production component, SLS gives you the mechanical honesty but not the cosmetic finish.
SLA: fine detail and clean surfaces
SLA cures resin with a laser or a light engine at layer heights a fraction of FDM’s. Edges come out crisp, small features hold their shape, and the surface is smooth enough to look finished straight off the machine.
The limits are mechanical. Standard resins are more brittle than nylon or ABS, and they degrade under UV light over time, so SLA parts are better suited to fit checks, visual models, molds and masters, and detailed enclosures than to load-bearing use. Engineering resins close much of that gap, but they still cost more per part than FDM.
How to choose
Work backwards from what the part has to do.
- Does it take a load, a bolt, or a drop? FDM in ABS, PETG, or PC, or SLS nylon.
- Does it have internal channels, overhangs, or moving joints? SLS.
- Does it need fine features, tight tolerances, or a smooth finish for review? SLA.
- Is it going into service at 20 to 500 units? SLS nylon is usually the most sensible route.
- Is it a first-article fit check? FDM or SLA, whichever gets you the answer cheaper.
Short runs without minimums
The old reason to pick a process was volume: injection molding only made sense above a few thousand parts, and tooling lead times decided the schedule. That trade-off no longer holds at the low end.
MultiplyParts runs FDM, SLS, and SLA under one roof in Canada, with no minimum order quantities. You upload your CAD file, get instant pricing, and move straight into production – one part or a short run, with no tooling to pay for and no offshore lead time to absorb. If a design changes at unit 30, you re-upload and reprint instead of writing off a mold.
That is the practical difference between the three processes: FDM for parts that work, SLS for parts that are complex and going into service, SLA for parts that have to look right. Know which one your part is, and the price you see on upload is the price that ships.
UPLOAD A PART. GET A PRICE. LAUNCH PRODUCTION.
